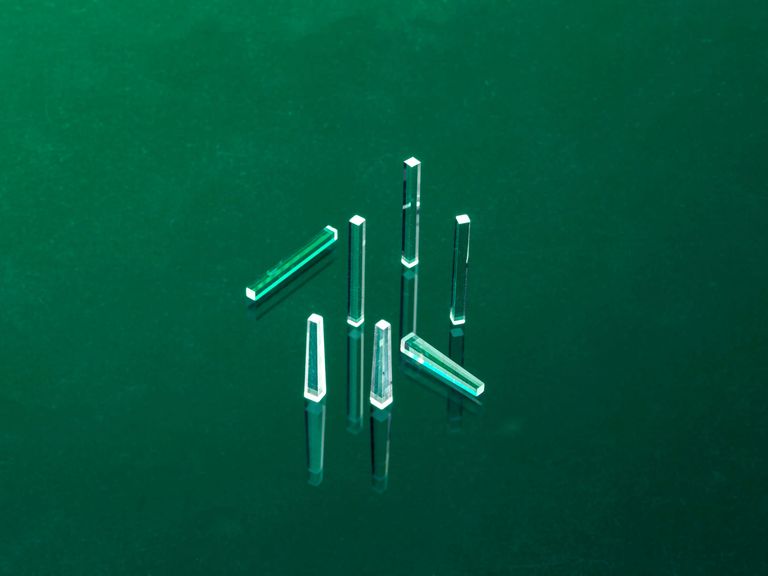
Square and rectangular
Straight or tapered light pipes for common rectangular illumination and sensor formats, the simplest to produce and to inspect.
IRD manufactures square, round, rectangular, hexagonal, and octagonal components in straight and tapered designs, with end faces held perpendicular or at a specified precision angle. Send the input beam and the output you need, and the technical team reviews it for manufacturability before quoting, free of charge on a new design.
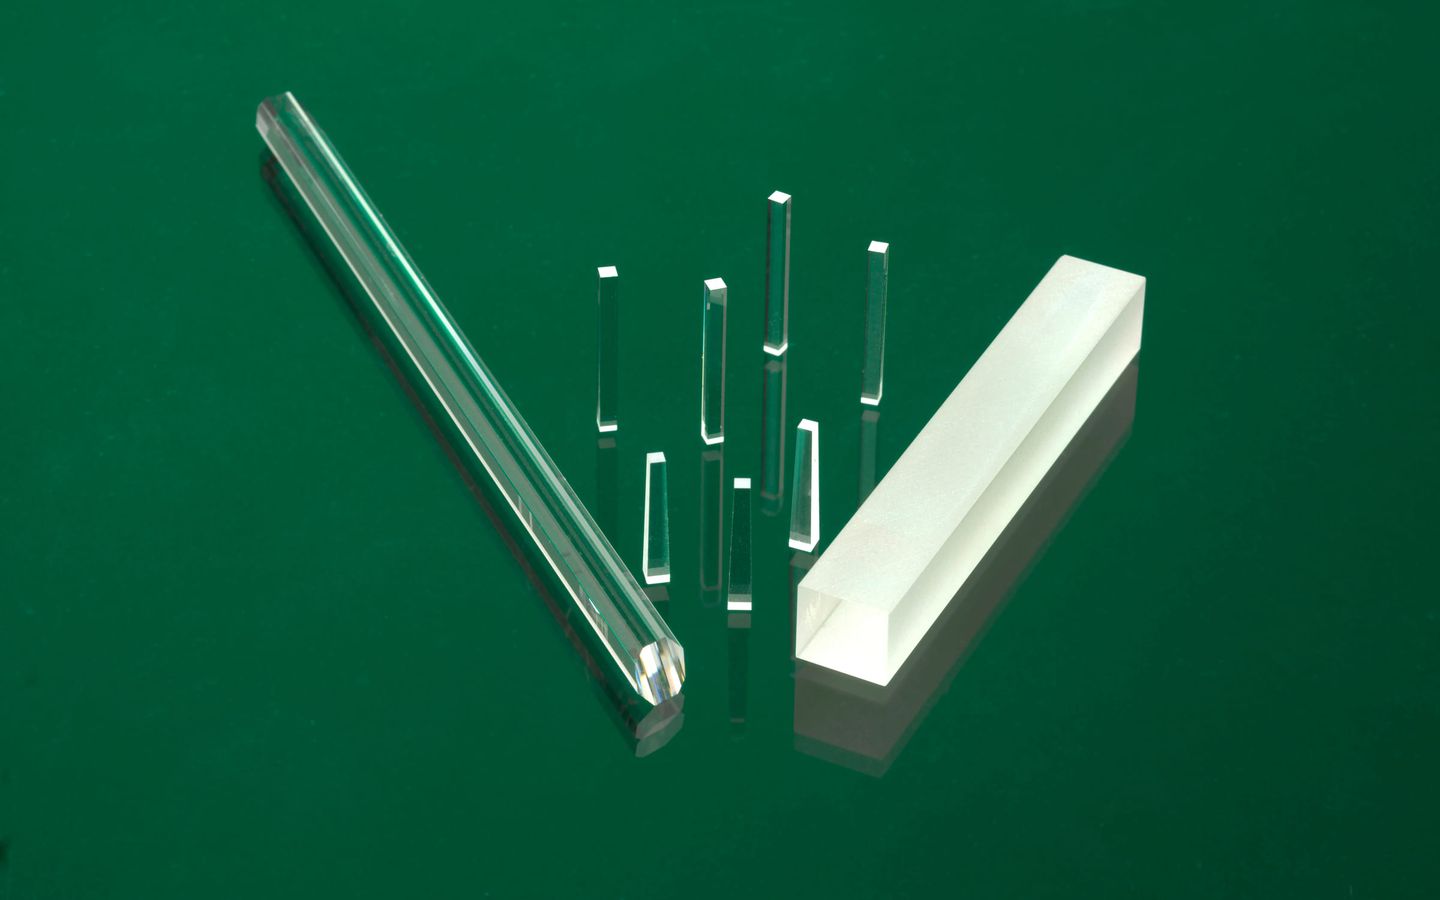
Cross section, taper, length, surface finish, entrance and exit faces, and material determine how the light mixes and how the component fits the system.
Straight or tapered light pipes for common rectangular illumination and sensor formats, the simplest to produce and to inspect.
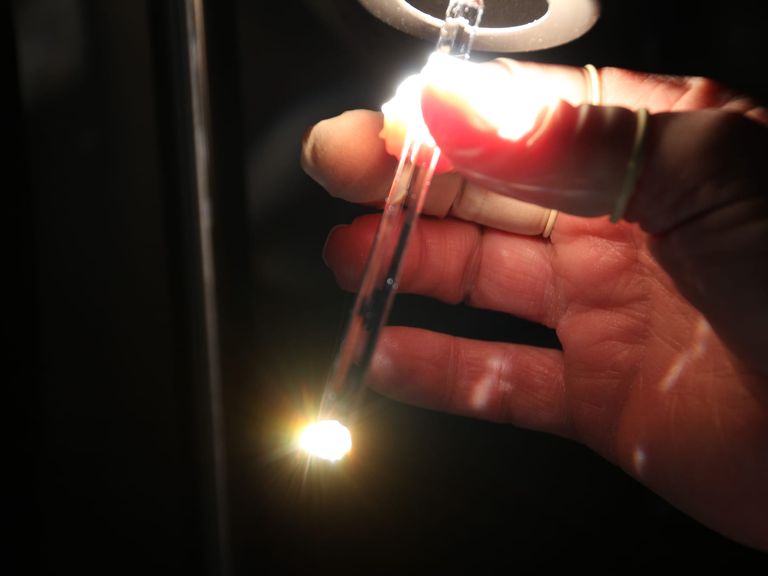
Cylindrical forms for compact beam delivery and assemblies built around circular mounts.
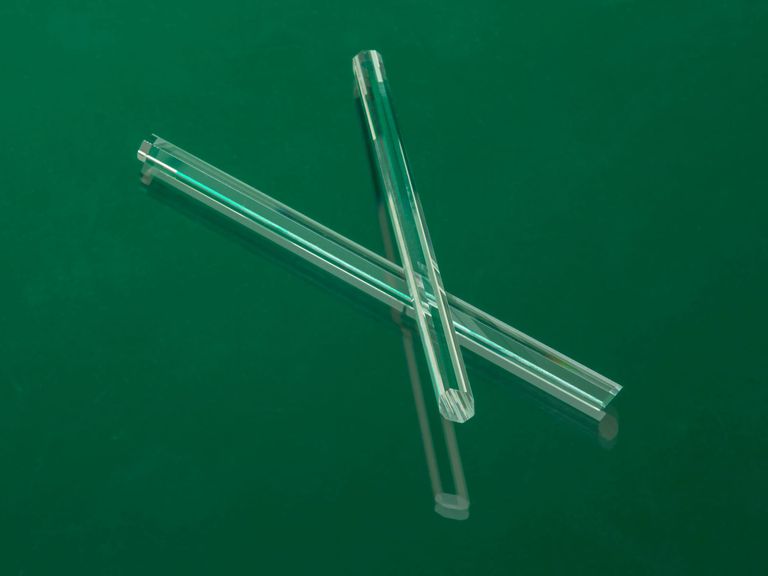
Multi-sided custom cross sections for specific mixing, packaging, and throughput requirements. More facets raise transmission and also raise handling and inspection cost.
A hexagonal cross section transmits about 35% more than an equal-size rectangular rod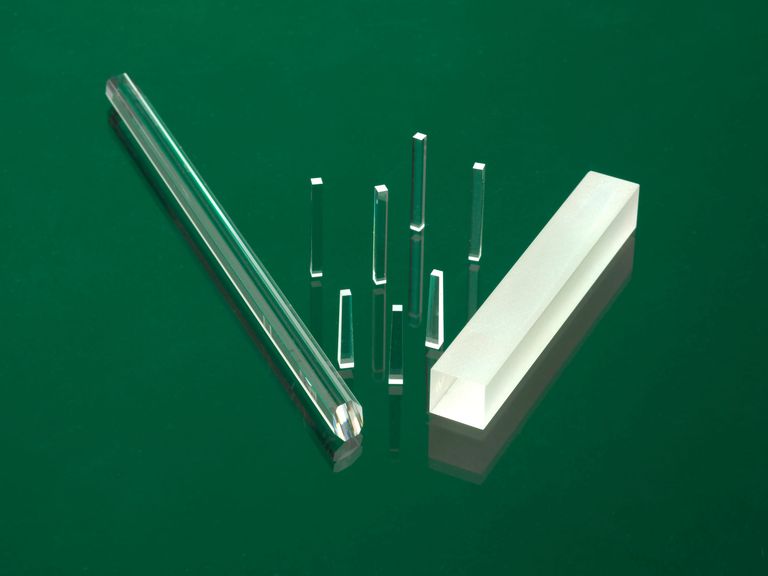
Entrance and exit faces manufactured perpendicular or at controlled angles, including Brewster-angle designs for polarized light, with custom coatings applied to end faces where optical noise matters.
These are IRD's published capability limits across materials and geometries, not a grade every part ships to. Open the process that controls your critical surface and quote against that one.
Homogenizer requirements are application-specific. Include the input beam, desired output, wavelength, material, envelope, face angles, and mounting scheme.
| Attribute | Typical | Best case |
|---|---|---|
| Surface flatnessWavefront-critical faces and mirrors | 1 wave | < 1/20 wave |
| ParallelismWindows, filters, and beam-steering optics | 30 arc sec | < 2 arc sec |
| Surface roughnessHigh-energy and scatter-sensitive applications | Ra < 1 µin | Ra < 2 Å |
| Dimensional toleranceFinished geometry and mounting interfaces | ±.005″ | ±.0001″ |
A homogenizer works because light stays inside it. Every scratch, pit, chip, and dimensional variation on a reflecting wall is a place for light to leave, which makes edge condition, not surface figure, the specification that usually decides the part.
Scratches or pits on planar surfaces, chips along edges, and even variations in surface dimensions all let light escape and cut efficiency. More facets mean more handling, and more handling means more opportunity to create the loss-inducing chip that was not there when the part was polished.
A hexagonal cross section provides roughly 35% greater transmission than an equivalent-size rectangular rod. An octagonal rod has twice the surfaces and edges of a rectangular one and is substantially more complex to produce, IRD manufactures them in volume, but the tradeoff belongs in the design review.
Input faces are usually made perpendicular to the side faces to make coupling easier. Output faces are often tilted to Brewster's angle to minimise reflection loss at that surface, and many designs carry a custom coating on the end faces to reduce optical noise in the system.
IRD's stated philosophy is to build quality into each operation rather than sort for it at the end, backed by investment in custom automation to reduce cost, more effective polishing processes to raise yield, and higher-precision inspection equipment.
IRD reports a zero parts-per-million defect rate over several yearsA major European laser manufacturer was struggling to secure reliable delivery of an octagonal homogenizer. The application handled laser beams of several kilowatts, so the design carried stringent surface and edge quality specifications, and the material was a very pure, low-loss, very brittle type of fused silica. Having already produced a different high-quality component for another business unit of the same manufacturer, IRD was asked to review the new application. It invested in a dedicated production cell with custom fixturing, new processes, and months of training in both manufacturing and inspection. Out of a 25-rod sample manually inspected at the customer's own European facility, only one chip larger than 30 microns was found across all the flat and angled edges.
Talk to an applications expertIRD's published materials, coating, and inspection equipment lists.
The answers an applications engineer would give you on the first call.
Start a quoteSquare, round, rectangular, hexagonal, and octagonal are all manufactured. IRD reports that a hexagonal cross section delivers about 35% greater transmission than an equivalent-size rectangular rod, so the shape is a performance decision rather than a cosmetic one.
It depends on what you need from the output. Tapered designs reduce the numerical aperture of the output, but tapered efficiency depends on dimensional precision, the better output costs more to produce. Say what the downstream optic needs and the team will scope both.
IRD's quoting checklist: application, product type, volume potential and schedule, material, dimensions, surface quality, coatings, assembly, cleaning, and packaging. Attach the drawing. For a new design the technical team runs a no-cost Design for Manufacturability review before quoting, then estimates prototype and production volumes separately.
No. IRD manufactures to your print or performance requirement and contributes material, process, and manufacturability input, the design stays with your team. When a print calls for tighter tolerances than the application requires, IRD will flag the potential over-specification, since it can add unnecessary cost. Final optical design decisions remain yours.
Machining runs to 30″ × 16″ × 16″, polishing to 36″ diameter, grinding to 24″ diameter at 6″ height, lapping to 13.3″ diameter, waterjet to 40″ × 24″ × 2″, and dicing to 8″ diameter at .300″ thick. Larger geometry is quoted against whichever process controls the critical surface.
IRD applies basic anti-reflective and metallic coatings in-house for quick turnaround. Other coating requirements are handled through select, vetted coating partners. Name the coating target in the RFQ and the team will confirm the route before quoting.
IRD is registered with the Directorate of Defense Trade Controls, and controlled programs are manufactured and stored domestically across the Litchfield and Alexandria, Minnesota facilities. Both plants operate under quality systems certified to ISO 9001:2015 and ISO 13485:2016 for ultra-high-precision glass, optical, and ceramic components.
Packaging is tailored to the part and can include multi-layer foam, custom corrugated packaging, gel packs for sensitive optics, and military-grade cases. Components are supported on edges or non-critical surfaces outside the clear aperture and held against shifting in transit.
Use these IRD references when reviewing laser homogenizers & light pipes requirements.
Legacy technical paper. Company-profile details may be outdated; use current site pages for IRD facts. IRD's account of the homogenizer design tradeoffs, cross section, taper, face angles, coatings, and surface and edge quality, why custom parts can beat stock on price at volume, and the multi-kilowatt octagonal case study in full.
PDFTechnical articleWhat a homogenizer does with total internal reflection, the applications it serves from display backlighting to wafer inspection, and the factors and specifications to fix before manufacture.
ArticleTechnical articleA practical selection walkthrough, light source, beam uniformity, illumination shape, assembly space, wavelength range, and inspection expectations, for teams deciding between catalog and custom.
Article
Send the input beam and the output you need, wavelength, material, cross section and whether it is straight or tapered, length and envelope, entrance and exit face angles, any end-face coating, the edge and surface specification with its acceptance method, annual volume, and mounting scheme. For a new design, the technical team runs a no-cost Design for Manufacturability review before quoting, then estimates prototype and production volumes separately.
Or call 320.693.7217. If you have a frozen design already in production and want a second source, IRD quotes that directly, the DFM review is optional, not a precondition.